Mostrando entradas con la etiqueta Toyota. Mostrar todas las entradas

viernes, 26 de junio de 2026

SMED: The Lean Technique That Can Transform Manufacturing Efficiency


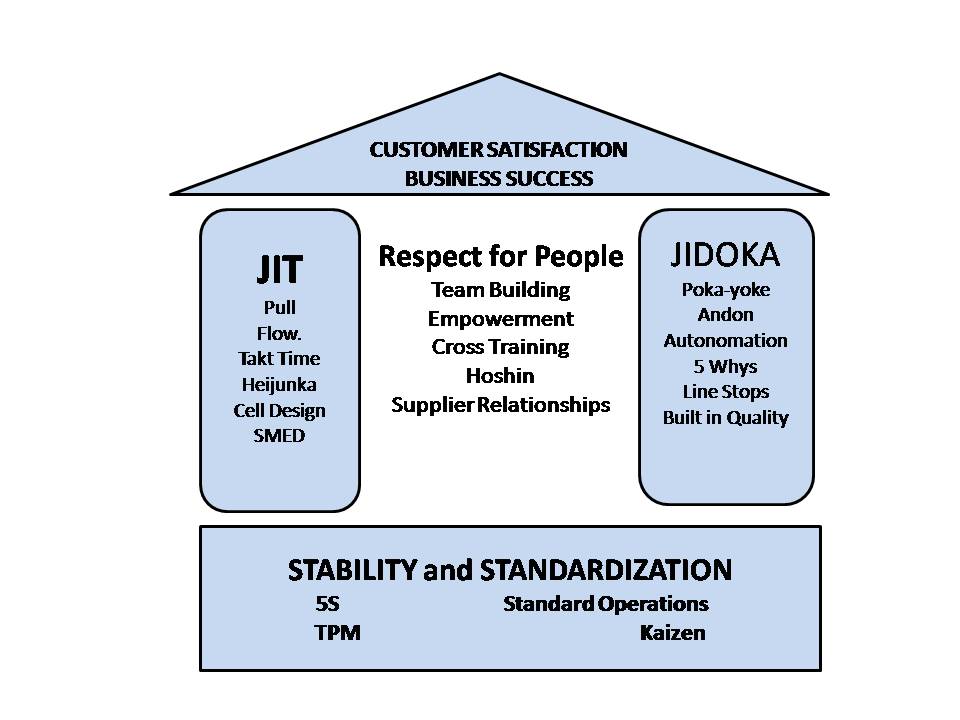
In today's competitive manufacturing environment, companies are constantly searching for ways to increase flexibility, reduce costs, and respond more quickly to customer demand. One of the most powerful Lean Manufacturing techniques for achieving these goals is SMED, which stands for Single-Minute Exchange of Dies.

Despite its name, SMED is not limited to changing dies in a press machine. It is a systematic methodology for reducing setup or changeover times in any manufacturing process. Whether switching between product models, adjusting machine settings, or preparing production lines, SMED helps organizations minimize downtime and maximize productivity.

What is SMED?

SMED was developed in the 1950s and 1960s by Japanese industrial engineer Shigeo Shingo as part of the Toyota Production System. The primary objective is to reduce setup times to less than ten minutes or at least make them dramatically shorter than before.

Long changeovers force manufacturers to produce large batches in order to justify the downtime. While this may seem efficient, it often results in excessive inventory, longer lead times, and reduced flexibility. SMED addresses this challenge by making changeovers so quick that smaller production batches become economically viable.

The SMED methodology follows three main steps:

1. Separate Internal and External Activities

Internal activities can only be performed while the machine is stopped, whereas external activities can be completed while the machine is still running. The first step is to identify each activity and determine whether it truly requires production to stop.

2. Convert Internal Activities into External Ones

Many tasks traditionally performed during downtime can actually be completed beforehand. Preparing tools, preheating equipment, organizing materials, or verifying settings before shutdown significantly reduces idle time.

3. Streamline Remaining Internal Activities

For the tasks that must occur during the changeover, the goal is to simplify and standardize every step. Quick-release fasteners, standardized tooling, parallel operations, and visual work instructions all contribute to faster and more consistent setups.

Reducing setup times delivers benefits that extend far beyond the production floor. Faster changeovers enable manufacturers to produce smaller batches without sacrificing efficiency, leading to lower inventory levels and improved responsiveness to customer demand.

Let´s see a simple example to illustrate this technique.

Imagine a packaging line that requires 90 minutes to switch from one product size to another. By analyzing the setup process, the team discovers that many tools are collected only after the machine stops, settings are adjusted manually, and operators perform tasks sequentially.

After applying SMED principles, tools are prepared in advance, machine settings are standardized, and two operators perform different tasks simultaneously. The result? The changeover time drops from 90 minutes to just 15 minutes. The company can now produce smaller batches, reduce inventory, and respond more quickly to changing customer orders.

SMED is more than a technique for speeding up machine setups, it is a mindset focused on eliminating waste and improving operational agility.

In a world where customer expectations continue to evolve and product lifecycles become shorter, the ability to change production quickly is a significant competitive advantage.

Whether you manage a large manufacturing facility or a small production line, implementing SMED can unlock hidden capacity, improve efficiency, and support a more responsive and resilient supply chain. Sometimes, the biggest improvements come not from working harder, but from making every minute count.


lunes, 30 de junio de 2025

Logistionary: Genchi Genbutsu


Genchi Genbutsu is a core principle of the Toyota Production System that translates to "go and see for yourself."

It emphasizes firsthand observation to understand situations deeply, solve problems accurately, and make informed decisions.

Instead of relying on second hand reports or data alone, leaders and team members are encouraged to go to the actual place where value is created, such as the factory floor, the customer site, or the development environment.

The Genchi Genbutsu approach involves:

  • Visiting the gemba: Physically going to the site of the issue or process.
  • Observing without assumptions: Understanding the facts directly through observation.
  • Engaging with people: Talking to employees, operators, or customers involved.
  • Asking “Why?” and using the “5 Whys” technique to get to the root cause.
 
Genchi Genbutsu promotes situational awareness, empathy, and fact-based leadership. It bridges the gap between strategy and execution, ensuring leaders stay grounded in operational realities.

Finally, a word to clarify the difference between Genchi Genbutsu and Gemba; Gemba means "the real place" where work happens and value is created (like a factory floor) Genchi Genbutsu means "go and see for yourself" and emphasizes firsthand observation to understand problems deeply.

Gemba is the location, Genchi Genbutsu is the mindset and method of investigation.


viernes, 27 de octubre de 2023

Logistionary: Kanban


Kanban is a visual scheduling system for lean manufacturing.

It all started in the early 1940s when the first Kanban system was developed by Taiichi Ohno for Toyota automotive in Japan. It was created as a simple planning system, the aim of which was to control and manage work and inventory at every stage of production optimally.

The Kanban method gets its name from the use of kanban, visual signalling mechanisms to control work in progress for intangible work products.

Kanban aligns inventory levels with actual consumption. A signal tells a supplier to produce and deliver a new shipment when a material is consumed. This signal is tracked through the replenishment cycle, bringing visibility to the supplier, consumer, and buyer.

In contexts where supply time is lengthy and demand is difficult to forecast, often the best one can do is to respond quickly to observed demand. This situation is exactly what a kanban system accomplishes, in that it is used as a demand signal that immediately travels through the supply chain.

Kanban cards are a key component of kanban, and they signal the need to move materials within a production facility or to move materials from an outside supplier into the production facility. The kanban card is, in effect, a message that signals a depletion of product, parts, or inventory. When received, the kanban triggers replenishment of that product, part, or inventory.

Three-bin system

An example of a simple kanban system implementation is a "three-bin system" for the supplied parts, where there is no in-house manufacturing. One bin is on the factory floor (the initial demand point), one bin is in the factory store (the inventory control point), and one bin is at the supplier. The bins usually have a removable card containing the product details and other relevant information, the classic kanban card.

When the bin on the factory floor is empty (because the parts in it were used up in a manufacturing process), the empty bin and its kanban card are returned to the factory store (the inventory control point). The factory store replaces the empty bin on the factory floor with the full bin from the factory store, which also contains a kanban card. The factory store sends the empty bin with its kanban card to the supplier. The supplier's full product bin, with its kanban card, is delivered to the factory store; the supplier keeps the empty bin. This is the final step in the process. Thus, the process never runs out of product, and could be described as a closed loop, in that it provides the exact amount required, with only one spare bin so there is never oversupply.

If all this is confusing, and you´re still not clear on how Kanban works, Im sure the next image will make everything fall into place! One image is indeed worth a thousand words as they say!


martes, 3 de octubre de 2023

Kaizen: All you need to know


Kaizen is a business philosophy that focuses on continuous improvement across the entire organization. The pursue of the kaizen model is to help companies focus on gradually and consistently increasing efficiency and reducing waste within processes. That doesn't mean alterations happen slowly. The kaizen process simply recognizes that small changes now can have huge impacts in the future.

To achieve all this, kaizen encourages input from any employee, from the factory floor to the most senior management.

The kaizen method became popular in Japan, at manufacturers like Toyota. Kaizen can broadly be translated as means continuous improvement in Japanese.

There are five fundamental Kaizen principles that are embedded in every tool and behaviour:

1. Know your customer

2. Let it Flow

3. Go to Gemba

4. Empower People

5. Be Transparent


Traditionally, kaizen has been known for its events, usually a three- to five-day team workshop in which employees, managers, and sometimes C-suite executives make an actionable plan to improve an existing process. Kaizen events often follow Gemba Walks or the discovery of an inefficiency. We have spoken about Gemba Walks in the past, these are visits to workplaces where management teams can witness processes, talk to employees, gather insights, and identify any issues. You can read more about Gemba Walks in here.

After you’ve identified problems or bottlenecks in a process, start making small, continuous improvements. During the kaizen event, team members collaborate and think of solutions. The ideal outcome of these events is an actionable plan that is ready for implementation.

Kaizen events can take many forms to best serve their business application.

1. Focused-improvement kaizen. A focused-improvement event is a kaizen event centred on a single, known issue. Prioritize your most important losses and develop solutions to eliminate them.

2. Waste kaizen. This type of event focuses on eliminating waste in your processes, as opposed to improving systems that are currently working.

3. Error-proofing kaizen. Use this type of event to reduce human error by improving processes. This could be as simple as standardizing checklists, automating parts of a system or using Poka Yoke which we talked about here.

4. Lead-time kaizen. This kind of event is suitable when you realize one of your processes is taking too long. The event aims to reduce the amount of time it takes to complete a process, like the time from processing an order to the customer receiving their goods.

How to run a Kaizen event:

There is not a unique way to conduct a kaizen event but the plan-do-check-act (PDCA) framework is common and often recommended method.


1. Plan

The Gemba Walk, mapping your value stream, and identifying the problems in your processes are part of the planning stage in a PDCA cycle. Follow these steps to get started.

  • Speak to employees. They’re the people who know the daily process better than anyone, so find out what problems or issues they're aware of.
  • Define and analyse the problem. When you’ve decided which issue to tackle, break it down and find the bottleneck in the process.
  • Establish the metrics you’ll use to measure success. Without this data it’s impossible to analyse the results after you’ve tested the solution.
  • Decide on a goal. You should have one goal that is achievable within the event time frame.
  • Work as a team to find solutions to the problem. There should be no limits on the kind of solutions encouraged. Allow employees to use their creativity. Choose one with potential to start with.


2. Do

Run a small-scale test of your chosen solution. Make sure every team member involved is aware of the change and let it run long enough to gather meaningful data and feedback.

3. Check

Collect data from your test and assess its success.

4. Act or adjust

If the test was a success, scale, implement your improved process company-wide or as a permanent update. However, if you found issues, or if the solution didn’t work, refine the process, and run further tests or choose a different solution and try again.

This should be a cyclical process. The kaizen event might be a one-time event but the process of improving never stops. To keep the continuous loop going, repeat the cycle. Find more processes to improve or try out other solutions
.

jueves, 3 de agosto de 2023

Logistionary: Kano model


The Kano model is a theory for product development and customer satisfaction developed in the 1980s by Noriaki Kano, a professor of quality management at the Tokyo University of Science.

It´s an approach to prioritizing features on a product roadmap based on the degree to which they are likely to satisfy customers. Product teams can weigh a high-satisfaction feature against its costs to implement to determine whether or not adding it to the roadmap is a strategically sound decision.

The model involves two dimensions:

1. Achievement (the horizontal axis), which goes from the supplier didn’t do it at all to the supplier did it very well.

2. Satisfaction (the vertical axis), which goes from total dissatisfaction with the product or service to total satisfaction with the product or service.

It also identifies three levels of customer expectations: that is, what it takes to positively impact customer satisfaction

1. Expected needs: These are the must haves, the requirements that the customers expect and are taken for granted.

These expectations are also known as the dissatisfiers because by themselves they cannot fully satisfy a customer. However, failure to provide these basic expectations will cause dissatisfaction.

Examples: In a hotel, providing a clean room is a basic necessity. In a call center, greeting customers is a basic necessity.

2. Normal needs: These are known as the wants or the satisfiers because they are the ones that customers will specify from a list. They can either satisfy or dissatisfy the customer depending on their presence or absence.

Examples: Time taken to resolve a customer's issue in a call center. Waiting service at a hotel.

3. Exciting needs: These are features and properties that make a supplier a leader in the market. These are the delighters or exciters because they go well beyond anything the customer might imagine and ask for. Their absence does not dissatisfy the customer, but their presence improves the likelihood of purchase.

Examples: In a callcenter, providing special offers and compensations to customers or the proactive escalation and instant resolution of their issue is an attractive feature. In a hotel, providing free food is an attractive feature.

How Does the Kano Model Work?

Using the Kano Model, product teams pull together a list of potential new features vying for development resources and space on the roadmap. The team will then weigh these features according to the two competing criteria:

1. Their potential to satisfy customers.

2. The investment is needed to implement them.


lunes, 15 de mayo de 2023

Hoshin Kanri: translating strategic plans into actionable items


Many companies struggle with translating strategic plans into actionable items on a daily process, luckily, among the most powerful tools in the Lean arsenal for effective strategic management we can find Hoshin Kanri.

Similar Jidoka or Just in Time, Hoshin Kanri has its roots in the Toyota Production System and as a tool, it can be very helpful, when implemented properly, in bridging the gap between strategy and execution.

Hoshin Kanri has a Matrix shape with four quadrants each devoted to a specific task.

1-     Set the strategic vision & goals (3-5 year breakthrough objectives):


The long-term goals is the starting point In Hoshin Kanri, normally in the frame between 3 and 5 years.


List them at the bottom quadrant of the matrix template and have in mind that every initiative will have many smaller tasks that will need to process before achieving the goal.


2-     Define key mid-term objectives (annual objectives)


After your long-term goals are all set, prepare the most important objectives that you aim to achieve in a shorter time frame and put them in the left quadrant of the Hoshin matrix.


3-     Set short-term actions and metrics (improvement priorities)


You will need to fill the top quadrant with the most important activities that need to be completed to achieve the short-term goals, this is basically the to-do list for the upcoming months.


4-     Agree on key performance indicators (targets to improve)


Agree on the most crucial metrics that need to be improved and list them on the diagram.


Following this line of thought, right next to the key metrics, you need to list the key stakeholders responsible for leading the completion of the activities in the matrix's top quadrant.


Finally, you should complete the picture by specifying the dependencies between every listing in your matrix.


domingo, 10 de septiembre de 2017

Just in time

Just-in-time manufacturing (JIT) also known as the Toyota Production System is a methodology aimed at reducing flow times within production systems as well as response times from suppliers and to customers.

It originated in Japan in the 1960s and 1970s, but the wise use of the term JIT faded in the 1990s as the new term “lean manufacturing” was established as a more recent name for JIT.

Benefits:

- Lower warehouse costs. Since less space is needed, this reduces the amount of storage an organisation needs to buy or rent.

- Less amount of inventory obsolescence, when companies use the traditional method of inventory they can end up with pallets of unsold items that simply go to waste

- Defect rates are reduced resulting in less waste and greater customer satisfaction.


Risks:


- You become reliant on your suppliers. Suppliers need to be able to supply materials quickly with very limited advance notice and any unexpected even can derive in long term out of stocks.

- Employees are at risk of precarious work as employers seek to easily adjust their workforce in response to supply and demand conditions by increasing the amount of contracting and temporary work.

- By not carrying much of stock, the risk of out of stocks is higher making imperative to have the correct procedures in place to ensure stock can become readily available.

- More and better planning is required to ensure stock is available at all times

If you want to learn more, check out the video below that explains in detail what JIT is and all the elements around this philosophy. 


Couldn´t finish this post without some music. Happy week!


miércoles, 9 de diciembre de 2015

Logistionary: Jidoka


Logistionary is back with new terms, definitions and concepts! And today it’s the turn for Jidoka.
For those of you that are familiarised with this term, there is still a lot to learn from this entry, for those that have never heard of Jidoka, watch out for what is one of the most important terms within the lean manufacturing environment.
First off, what is Jidoka, and why most of these terms have Japanese names?
Jidoka is the often forgotten pillar of the Toyota Production system but yet one of the most important, and the one that actually was a breakthrough in terms of achieving true excellence in manufacture.

Now, why most of these terms have Japanese names? Well, because they all actually were coined by the same person, Sakichi Toyoda, the founder of Toyota Industries, and the person that revolutionised the rudimentary logistic processes of that time. 


Coming back to the term that concerns us; Jidoka began with the invention of a simple device that could stop the shuttle on an automatic loom should the thread broke. This will prevent the machine from not only creating defects but also alerted the operator of a problem. This meant that now the operator could operate several machines at the same time and not only focus on just one in case something went wrong. This principle became known as “automation with a human touch”


Jidoka is based in 4 very simple principles:
  1. Discover an abnormality
  2. Stop
  3. Fix the immediate problem
  4. Investigate the root cause and correct


These principles are not just confined to use of machines, but they are visible in almost every aspect of lean manufacturing. It’s about building quality into a process rather than having to inspect the outcome at the end of the process.
Every individual in a lean company is allowed and actually is expected to stop the process should they discover an abnormality, this way problems are highlighted and actions to solve them are taken. This is a concept many western companies find hard to implement as they fear a loss in productivity derived from lines being constantly stopped. This fear however undermines the core principle of Jidoka which is investigating the root causes of problems and working on tackling them.
Even though stopping the lines might seem contra intuitive, in the long term the number of line stops begins to reduce as problems are removed and productivity begins to improve as root causes of problems are removed.
Within companies such as Toyota line stop is a way of life, if an operator detects a problem they pull a cord or push a button to stop the production line at the end of that production cycle. This alerts the team leader or supervisor who will immediately rush over to help solve the problem. If it can be easily corrected then they do so and restart the line, otherwise they call in whatever support is required to solve the problem.
The major obstacle to implement Jidoka and any other lean principles is the fear of the short term implications when stopping the lines, but once this concerns are overcame Jidoka has proven to be a major advantage in adding value and increasing productivity across all lines.
I hope you enjoyed this entry and you learnt something new. Watch this space for more interesting concepts in the near future!


domingo, 13 de septiembre de 2015

Logistionary: Heijunka


Heijunka means sequencing or smoothing of production. It has been definied as: “Leveling the type and quantity of production over a fixed period of time. This enables production to efficiently meet customer demands while avoiding batching and results in minimum inventories, capital costs, manpower, and production lead time through the whole value stream”.

The goal of this technique developed by Toyota as a mean to standardise work, is to produce intermediate goods at a constant rate so that further processing may also be carried out at a constant and predictable rate. This is achieved by switching from a line dedicated to a single product, which is therefore sensitive to sales variations, to a flexible line capable of manufacturing several types of product.

Some of the advantages of leveling production are:

  • Flexibility to make what the customer wants when they want it.
  • Reduced risk of unsold goods.
  • Balanced use of labor and machines.
  • Smoothed demand on the upstream processes and suppliers

The video below explains in detail production levelling, but if you still want a more thorough explanation check the second video out!